Quality &Food Safety
SQF CertifiedPlants & Facilities
AAFCO RegulatedSafety Practices
contact@sunshinemills.com
800-633-3349
Our Higher StandardsLet You Worry Less
At Sunshine Mills, quality and food safety are fundamental to everything we do. From ingredient sourcing and product development to manufacturing, testing, and distribution, we maintain rigorous programs designed to support product integrity, regulatory compliance, and customer confidence.
Our commitment to quality is backed by experienced professionals, advanced laboratory capabilities, industry-recognized certifications, and comprehensive food safety systems that help ensure consistency across every product we manufacture.
Quality Assurance Expertise
Our Quality Assurance team includes trained professionals with expertise and years of experience in food chemistry, food safety, microbiology, and quality systems management. Leveraging current technologies and established analytical methodologies, our team works to maintain high standards throughout every stage of the manufacturing process.
From ingredient evaluation and process verification to finished product assessment, our specialists are dedicated to supporting safe, consistent, and high-quality products.
Comprehensive Monitoring & Oversight
Quality is monitored throughout our operations to help ensure compliance with regulatory requirements, customer specifications, and internal standards.
Our Quality team oversees the facilities, equipment, environmental conditions, personnel practices, manufacturing methods, records, and control systems that contribute to product quality and food safety. Through ongoing monitoring and verification activities, we strive to maintain operational excellence across our manufacturing network.
Advanced Testing & Laboratory Analysis
All product analysis is conducted within secured, access-controlled facilities designed to support accuracy, reliability, and data integrity.
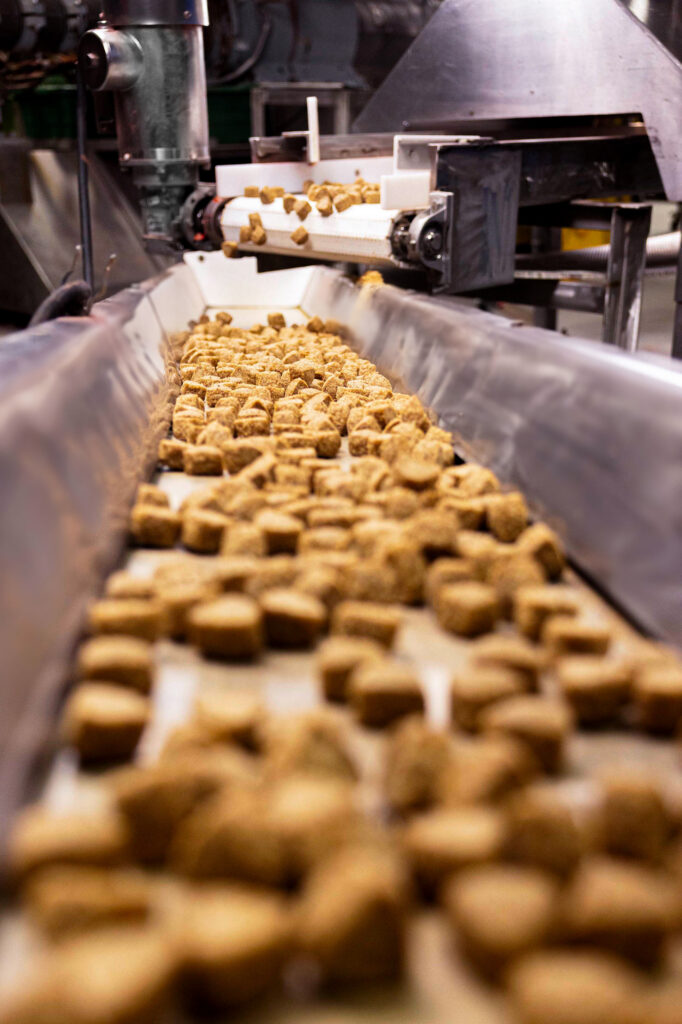
Each manufacturing facility is supported by an on-site satellite laboratory operating with 24/7 support capabilities and state-of-the-art analytical instrumentation. These resources allow our teams to perform timely testing and evaluation throughout production, helping verify product quality, safety, and consistency.
SQF Certified Manufacturing
Our manufacturing facilities operate under Safe Quality Food (SQF) certification programs, one of the most recognized and respected food safety and quality management systems in the world.
SQF certification demonstrates our commitment to maintaining robust food safety practices, continuous improvement, risk management, and regulatory compliance throughout our operations. Through regular audits and ongoing program management, we work to ensure our facilities consistently meet the highest standards of quality and safety.
AAFCO Compliance
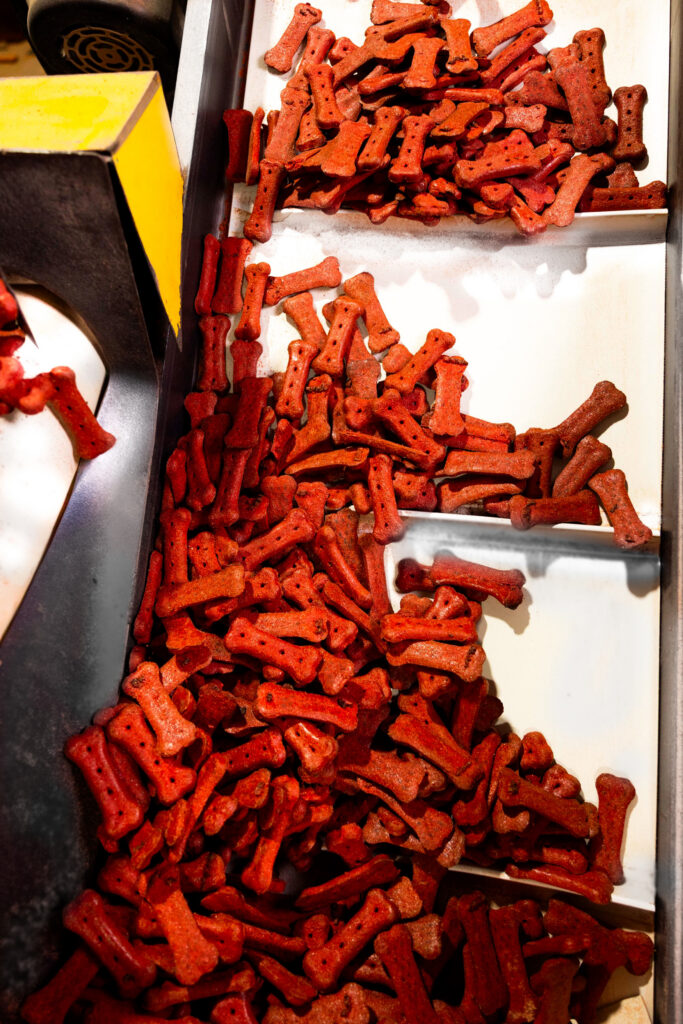
We formulate and manufacture products in accordance with applicable guidelines established by the Association of American Feed Control Officials (AAFCO).
By adhering to recognized nutritional and labeling standards, we help ensure products are developed with consistency, transparency, and compliance in mind, providing confidence for both our customers and the consumers they serve.
Safety Programs thatSupport Every Product
Our quality management system is built upon a comprehensive framework of programs and controls that support food safety, regulatory compliance, and continuous improvement. Together, these programs help ensure that every product manufactured by Sunshine Mills is supported by consistent processes, rigorous oversight, and a commitment to quality at every stage.
Analytical Verification
Routine product sampling and analytical testing help verify product quality, safety, and consistency in accordance with established specifications and manufacturing standards.
Food Legislation
Our teams monitor and follow applicable food safety regulations and industry requirements to help ensure products are manufactured in compliance with current standards and guidelines.
Validation of Effectiveness
We routinely evaluate and validate the effectiveness of key food safety and quality processes to help ensure programs are operating as intended and supporting continuous improvement efforts.
Product Traceability
We maintain product traceability systems designed to support accurate tracking of ingredients, packaging, and finished goods throughout the production and distribution process.
Food Safety Plan
We maintain comprehensive food safety plans designed to identify, evaluate, and manage potential risks throughout the manufacturing process. These programs support a proactive approach to product safety and operational control.
Foreign Material Control
We utilize foreign material prevention and detection programs designed to help minimize contamination risks and support product safety throughout the manufacturing process.
Supplier Approval
We utilize supplier approval and monitoring programs to evaluate ingredient and material providers based on quality, safety, and compliance standards. This process helps support the integrity and consistency of incoming materials used in production.
Calibration Monitoring
Calibration monitoring procedures help ensure that critical instruments and measurement devices remain accurate and reliable to support product quality and process consistency.
Document Control
We maintain structured document control procedures to help ensure that policies, specifications, records, and operational documents remain accurate, current, and accessible throughout our facilities.
Food Quality Plan
Our food quality programs are focused on maintaining product consistency, performance, and customer expectations across all stages of manufacturing and packaging.
Food Defense
Our food defense programs are designed to help protect products, facilities, and supply chains from intentional adulteration or unauthorized access through controlled security and monitoring practices.
Training
We provide ongoing employee training programs focused on food safety, quality, operational procedures, and continuous improvement to help maintain high manufacturing standards across our facilities.
Pest Control
Integrated pest management programs are implemented throughout our facilities to help maintain sanitary manufacturing environments and support food safety standards.
Sanitation
Our sanitation programs include structured cleaning and verification procedures designed to maintain hygienic production environments and support safe manufacturing practices.
Our investment in food safety, quality systems, laboratory capabilities, and operational excellence helps provide the confidence that products are being manufactured with care, consistency, and integrity.
A Commitmentto Partnership
When customers choose Sunshine Mills as their manufacturing partner, they are choosing a company that understands the importance of protecting both product quality and brand reputation.